Industrial Conveyor
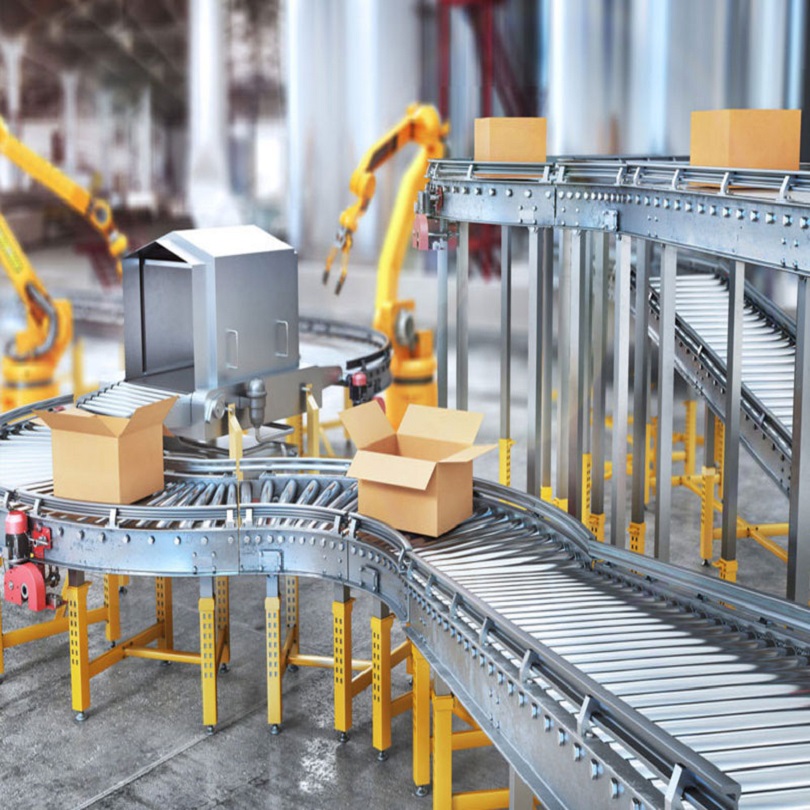
Industrial conveyors are mechanical material-handling systems that transport products, raw materials, or packages along a fixed path within a facility.
Key Uses and Benefits
- Efficiency: Speeds up cycle times and eliminates manual transport.
- Safety: Reduces heavy lifting and lowers workplace injury risks.
- Applications: Vital across bulk material handling, automotive assembly, food processing, and warehouse logistics.